These are not four services: they are four capabilities built in-house over years of investment which, taken together, explain why a Scame component costs less than its equivalent assembled from three separate parts. We describe them in the detail a design engineer needs in order to judge whether they apply to their component.
Technologies
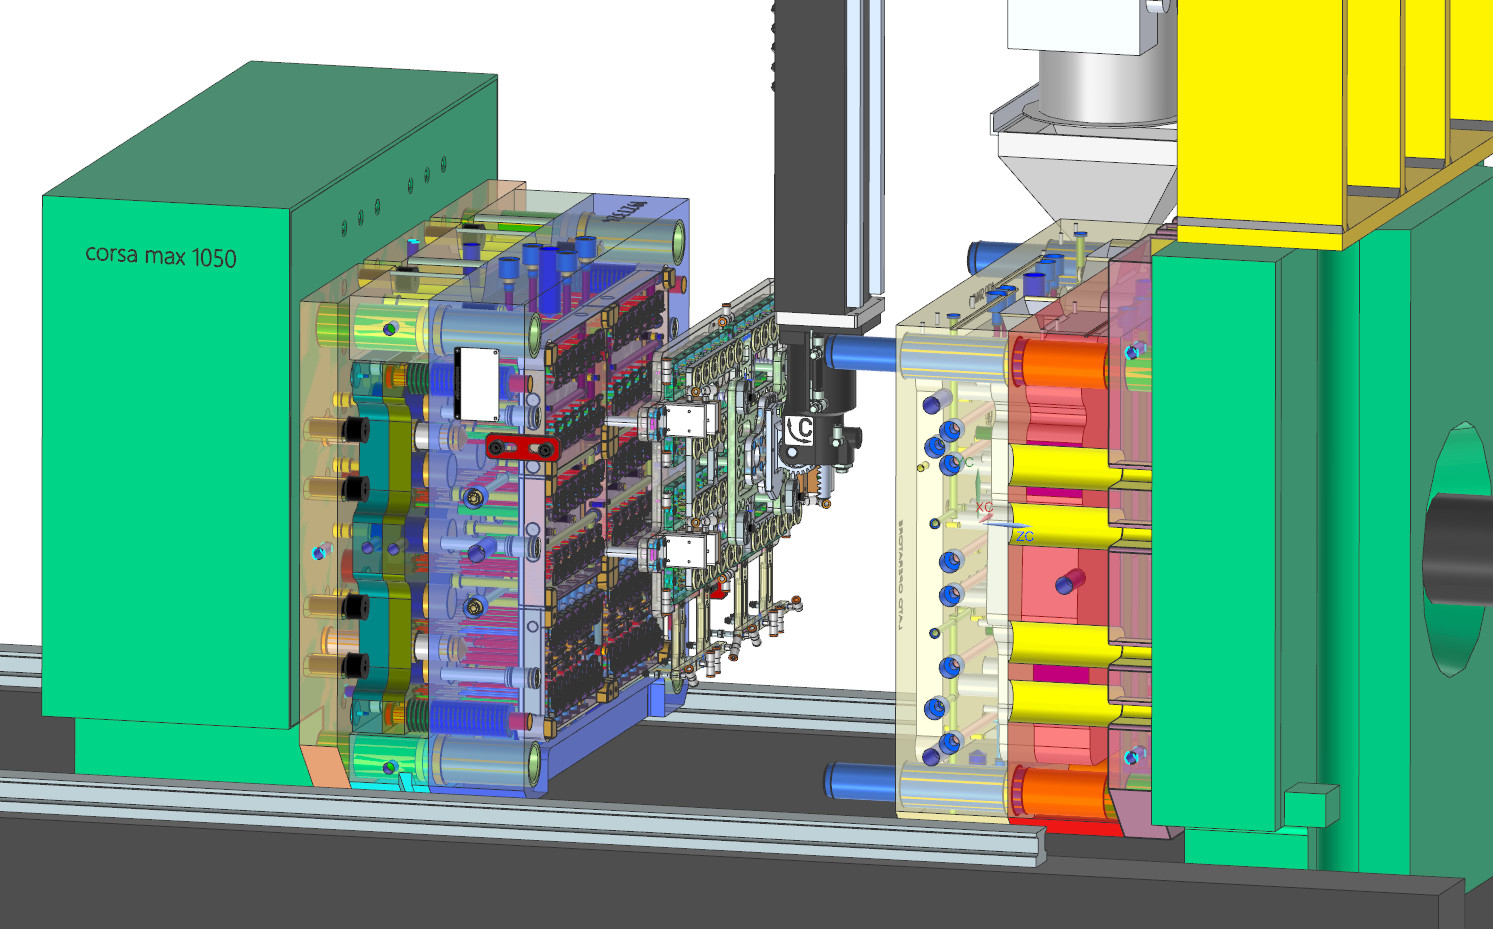
Multi-material moulding up to 6K, six different materials
Sequential or simultaneous injection of up to six polymers or colours in a single production cycle. This is a rare capability in the Italian and European plastics contract manufacturing sector: most competitors mould in a single colour and leave assembly to the customer.
The result is a component that leaves the machine assembly-ready and replaces three or four parts. Fewer part numbers in stock, fewer assembly operations, fewer potential defect points, and a single supplier accountable for the functional result. The assessment should be made on the total cost of the component, not on the unit price.
Configurazioni
6K, from the German Komponenten: six materials injected in a single cycle.
2K
3K
4K cell
Isola avanzata 6K
Proprietary automation and 100% inspection
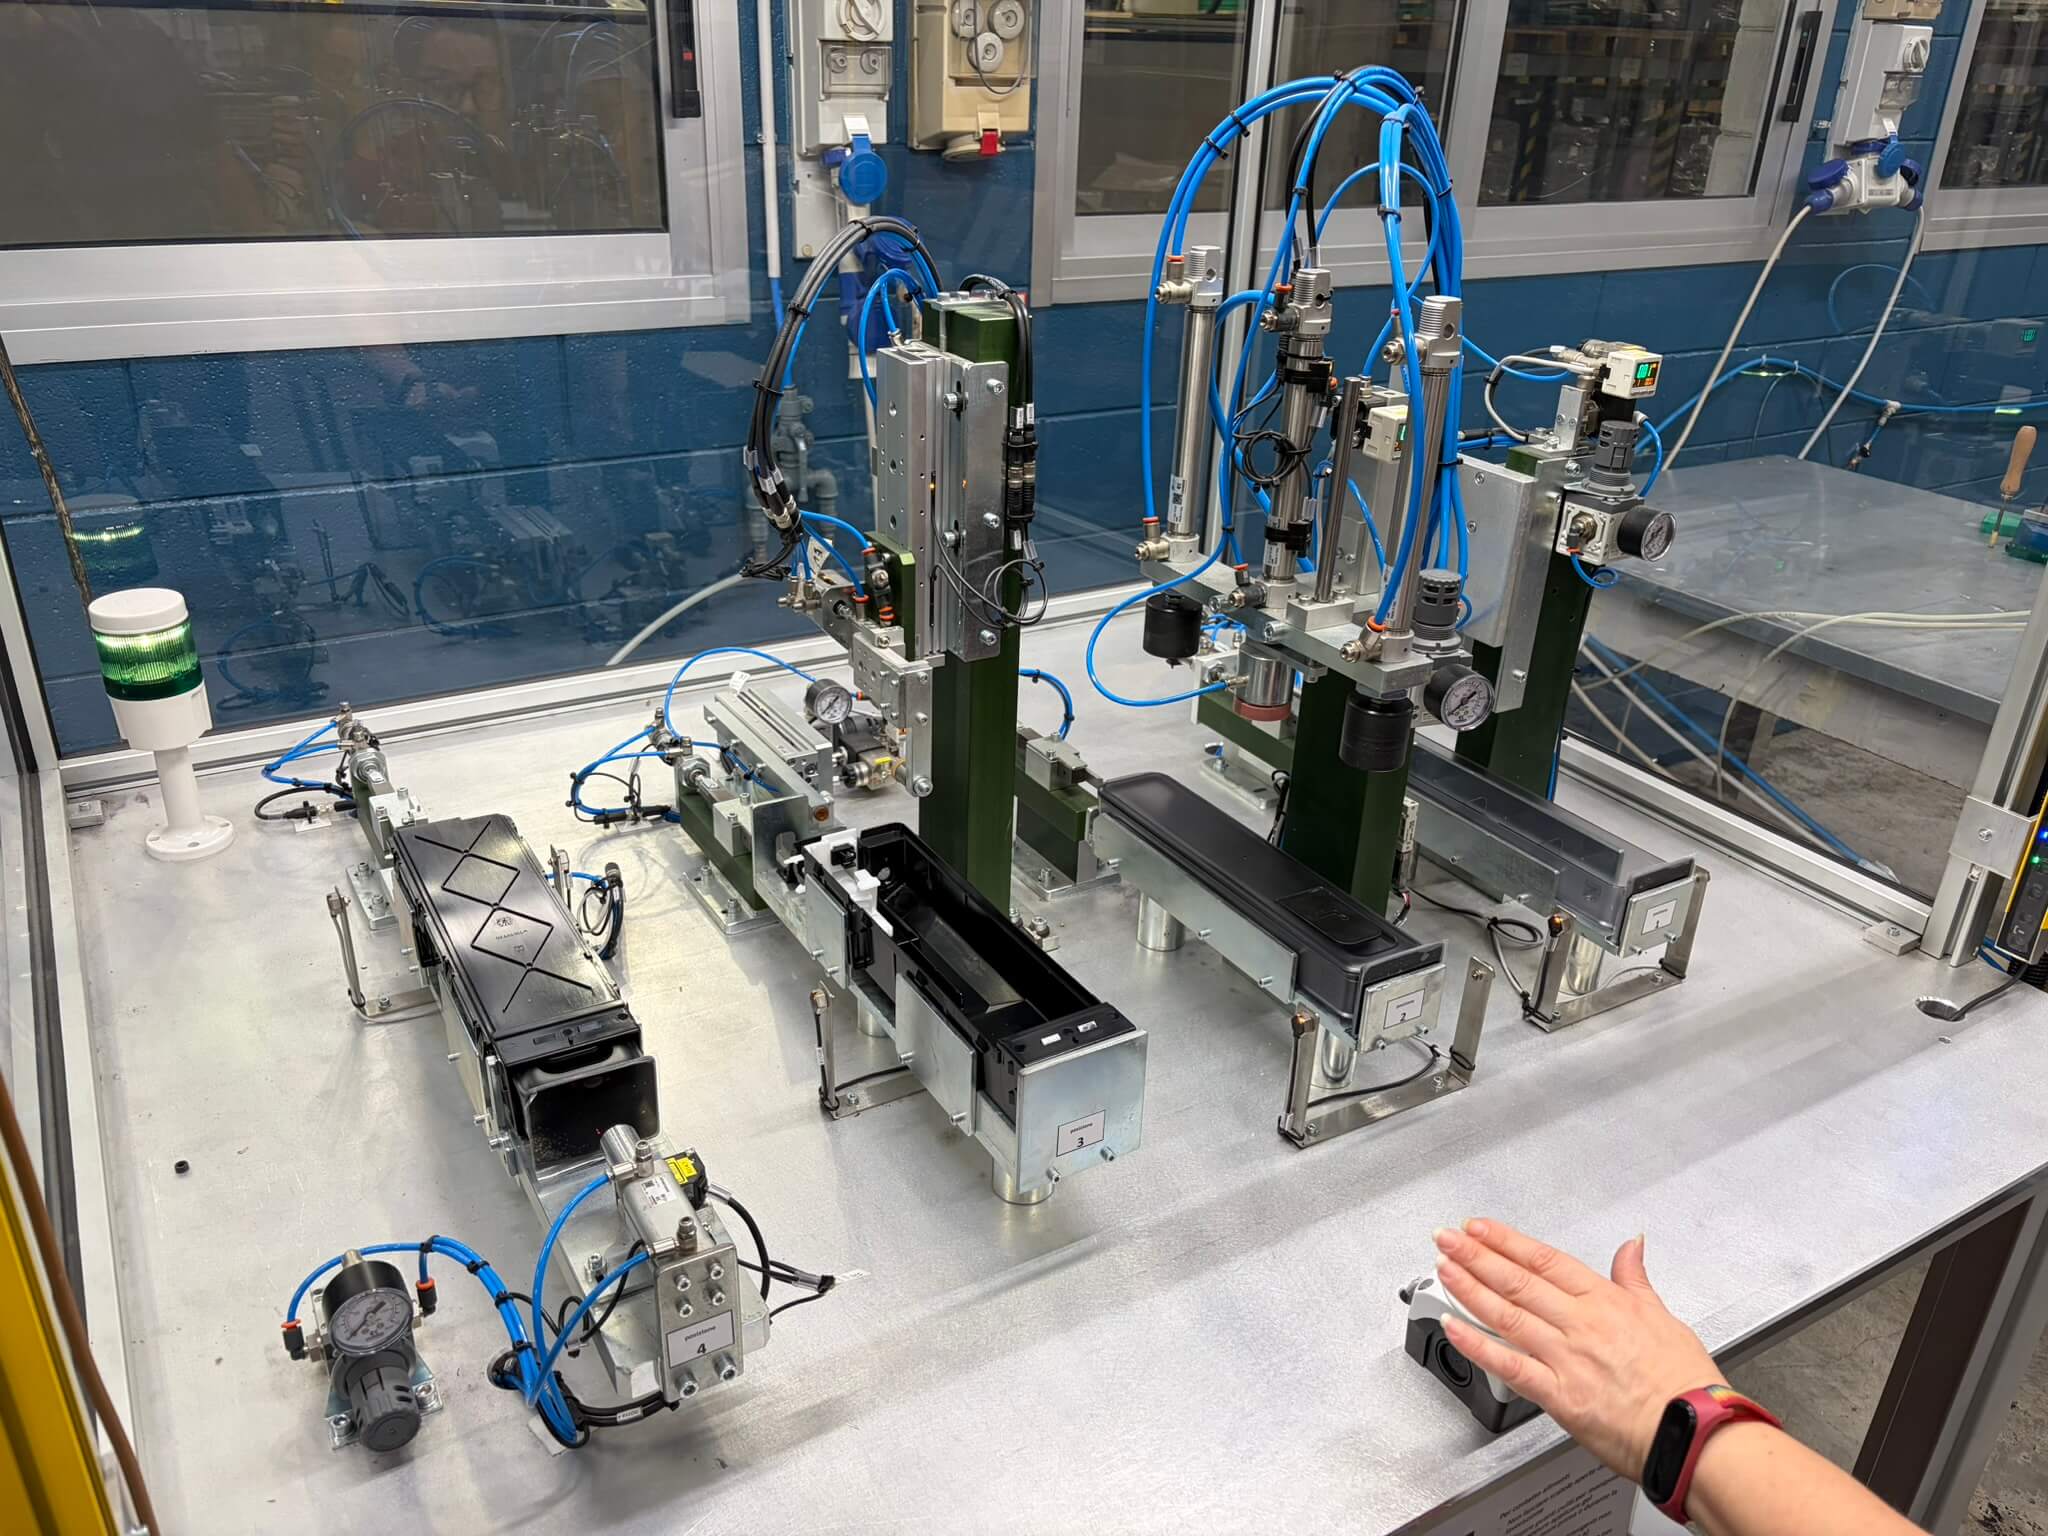
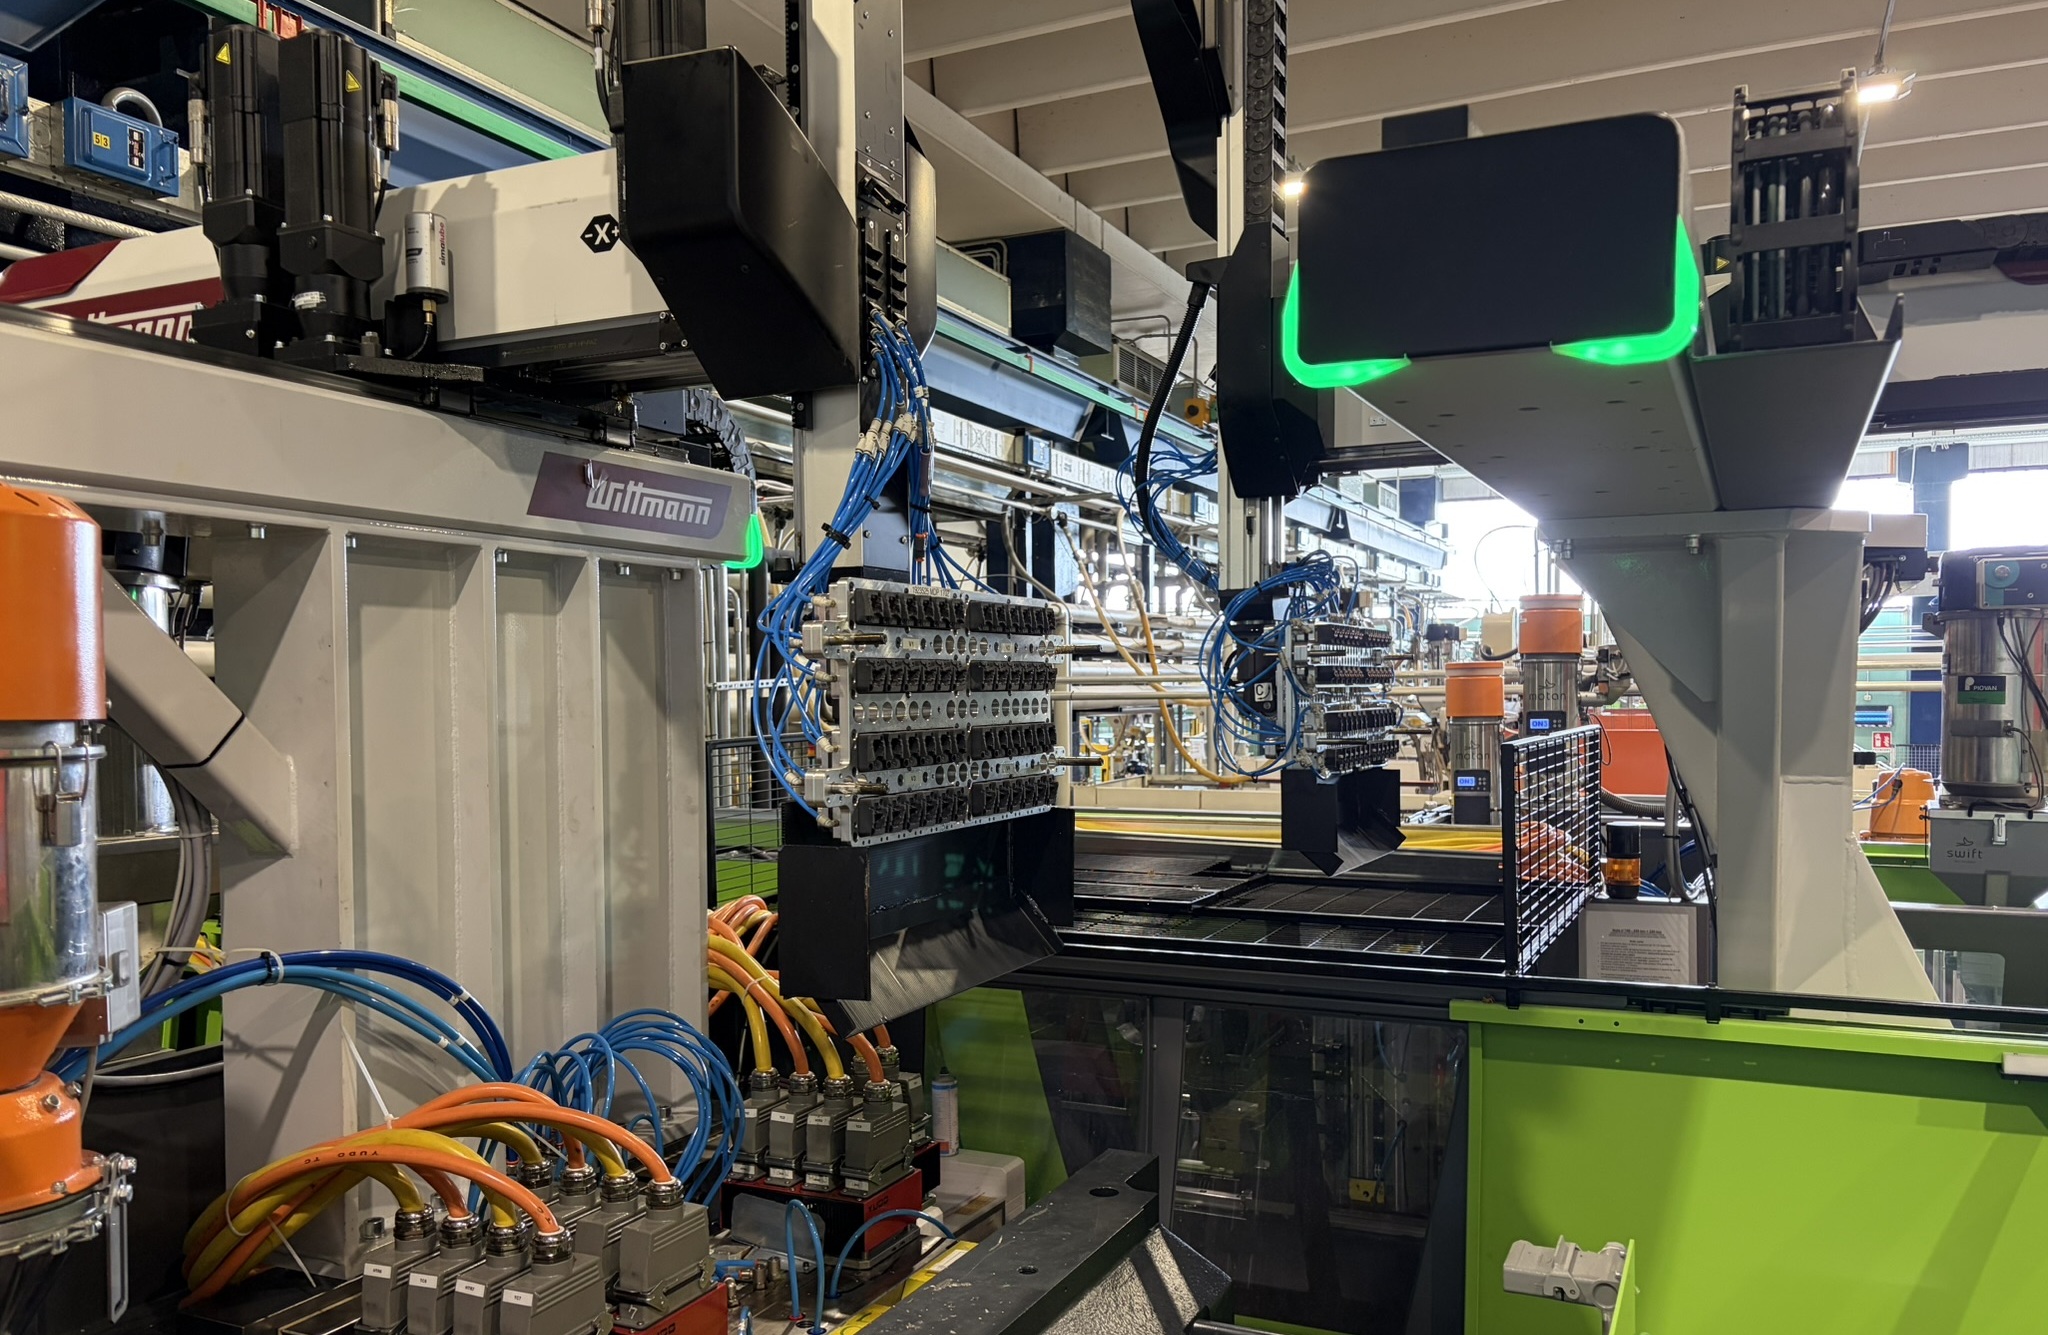
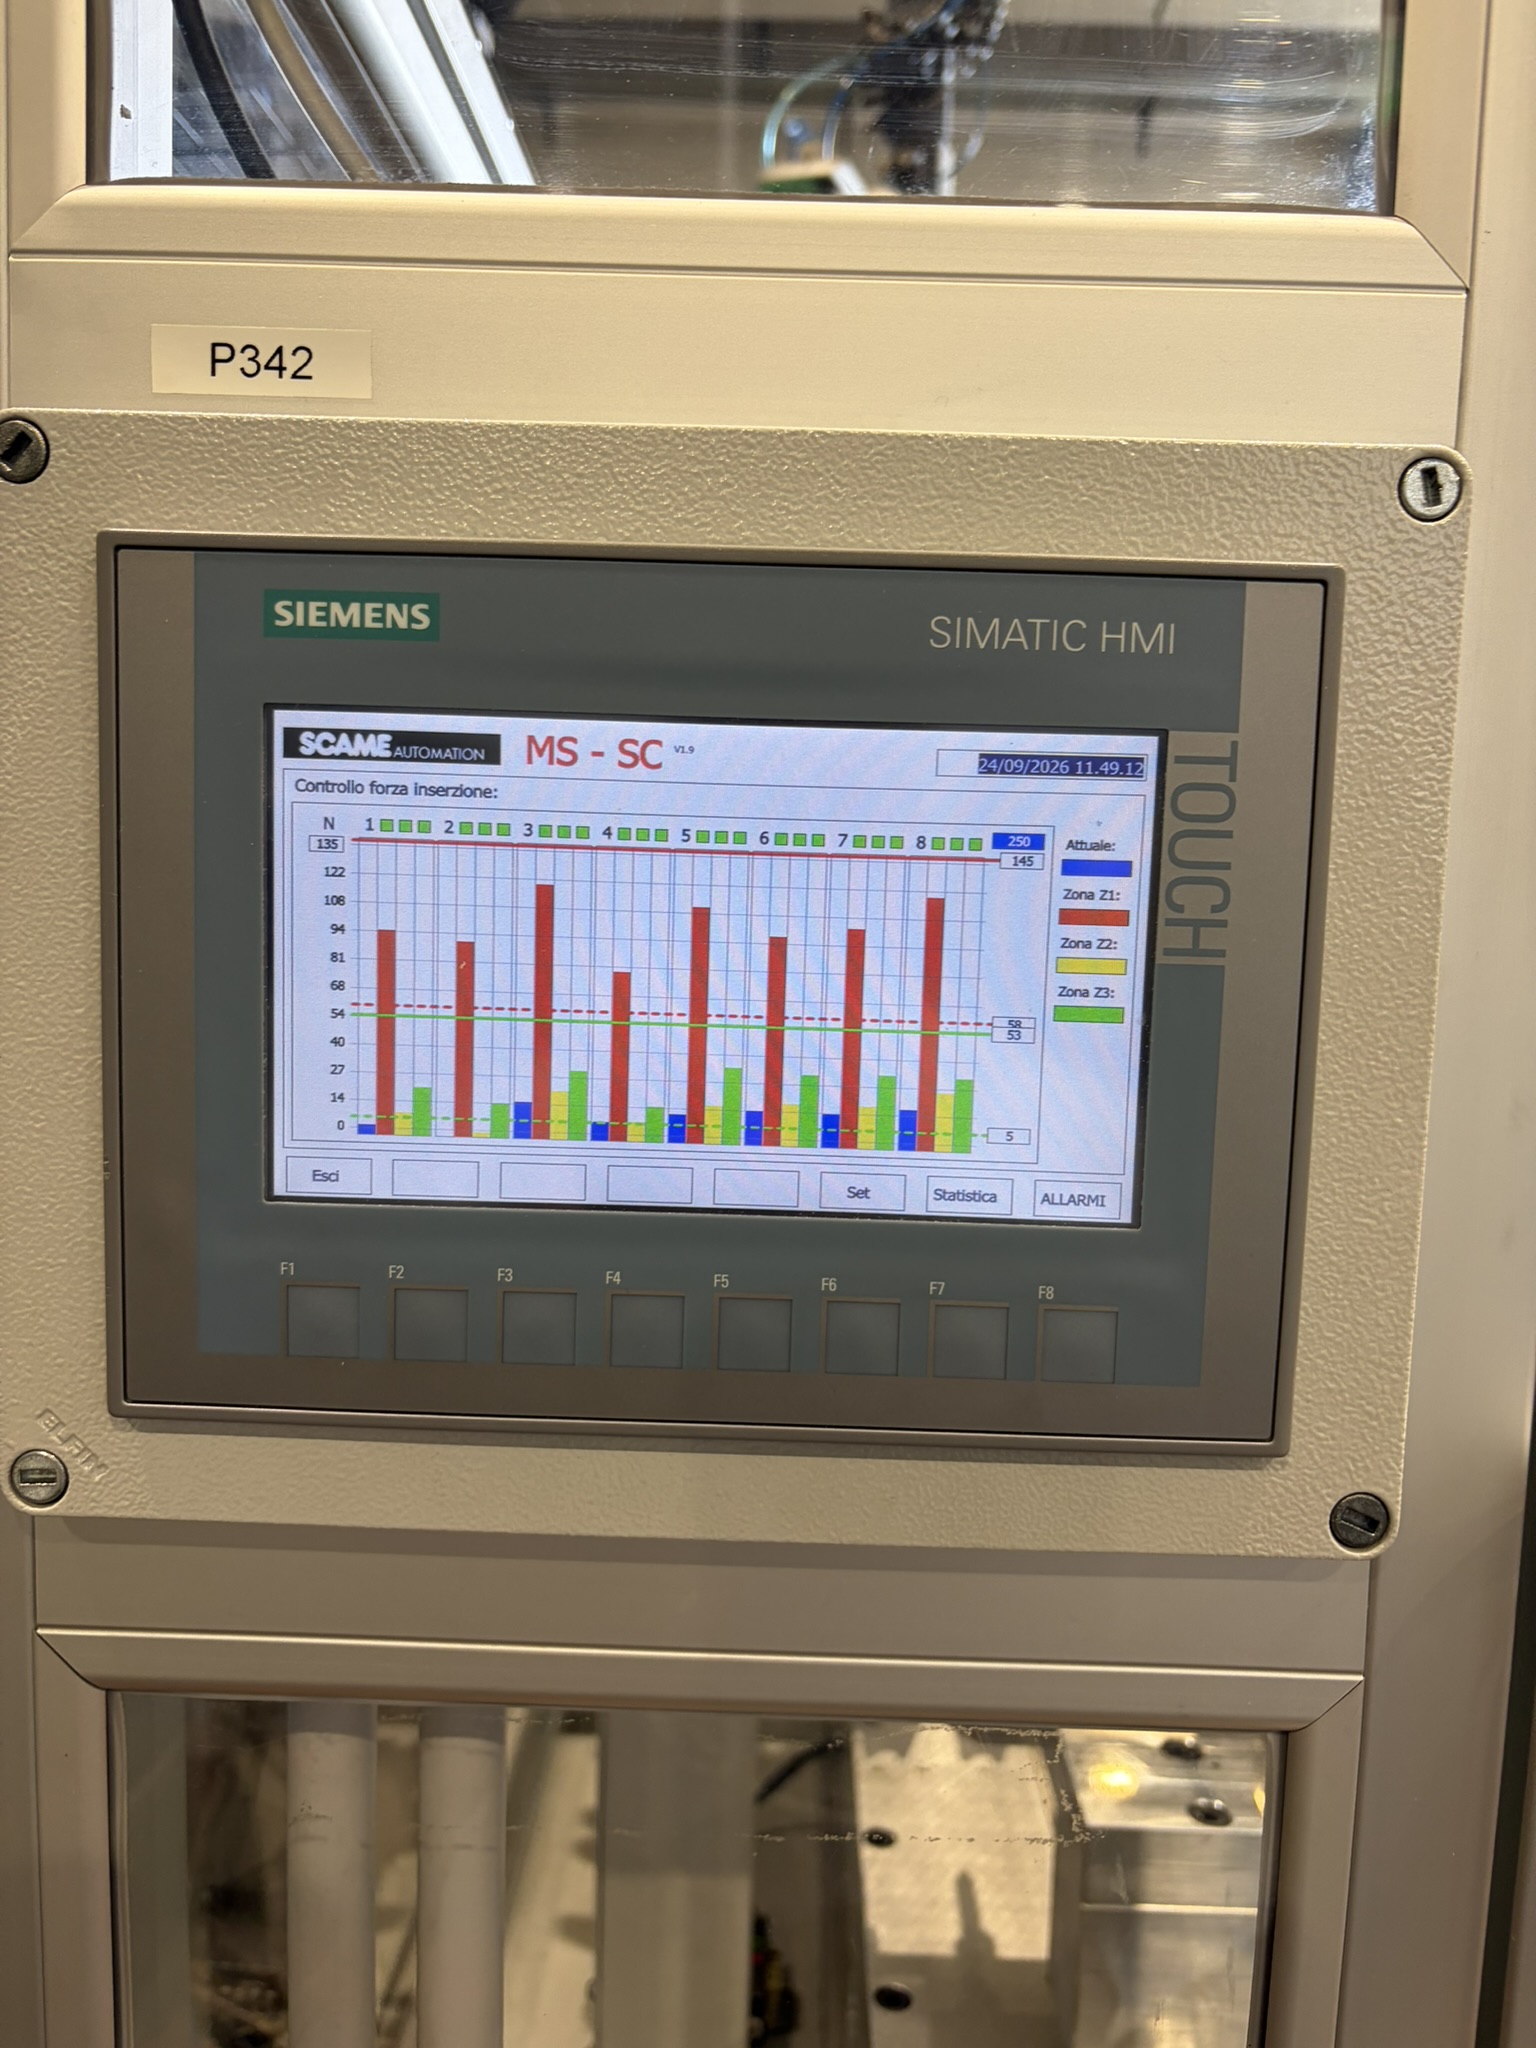
Pre-assembly cells at the moulding machine, designed and built in-house: insertion force monitoring on every part, 100% machine vision inspection, and twelve dual-head ultrasonic welding units with energy control.
Our cells are not bought in: they are designed and built in-house. That means we can adapt them to your functional specification, instead of asking you to adapt your component to standard automation. On medical projects the cell produces a complete Device History Record for every part.
Lights-out Industry 4.0 toolroom
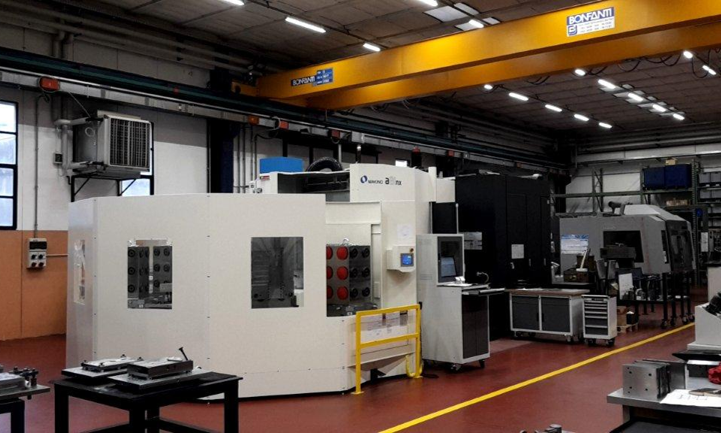
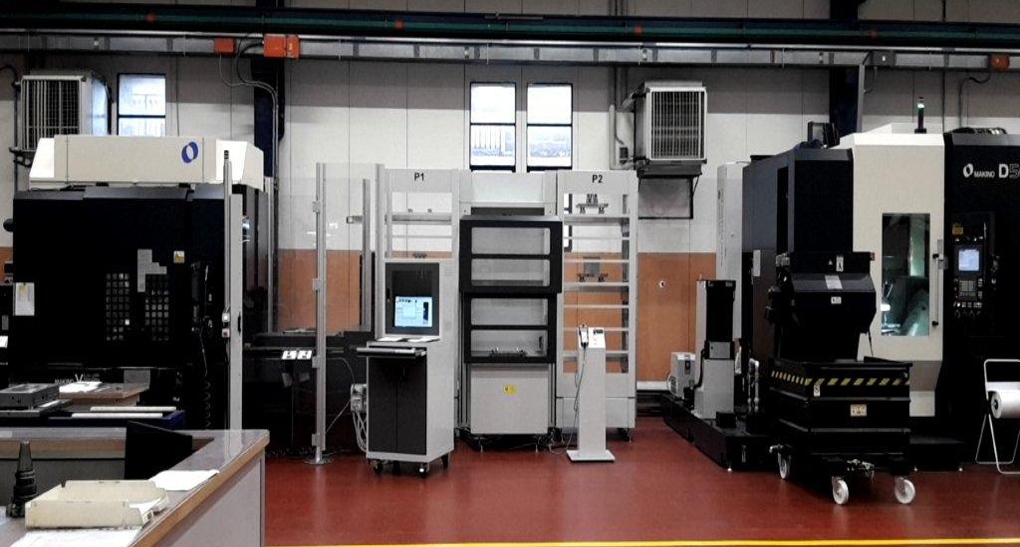
The toolroom is part of the Group, operates under the Cospa brand and builds standard moulds in four to six weeks. The cycle integrates MES and 3D presetting: offline tool loading while the CNC machine keeps running, 3D measurement before assembly, automatic transfer of offsets to the MES, unattended night-shift production and batch-by-batch traceability.
For a customer this means two things: mould construction lead times that do not depend on a third-party supplier, and process documentation available within 48 hours in the event of an ISO 13485 audit — retrieved from the system in minutes, rather than searched for in the archives over days.
Filter expertise and overmoulding of meshes
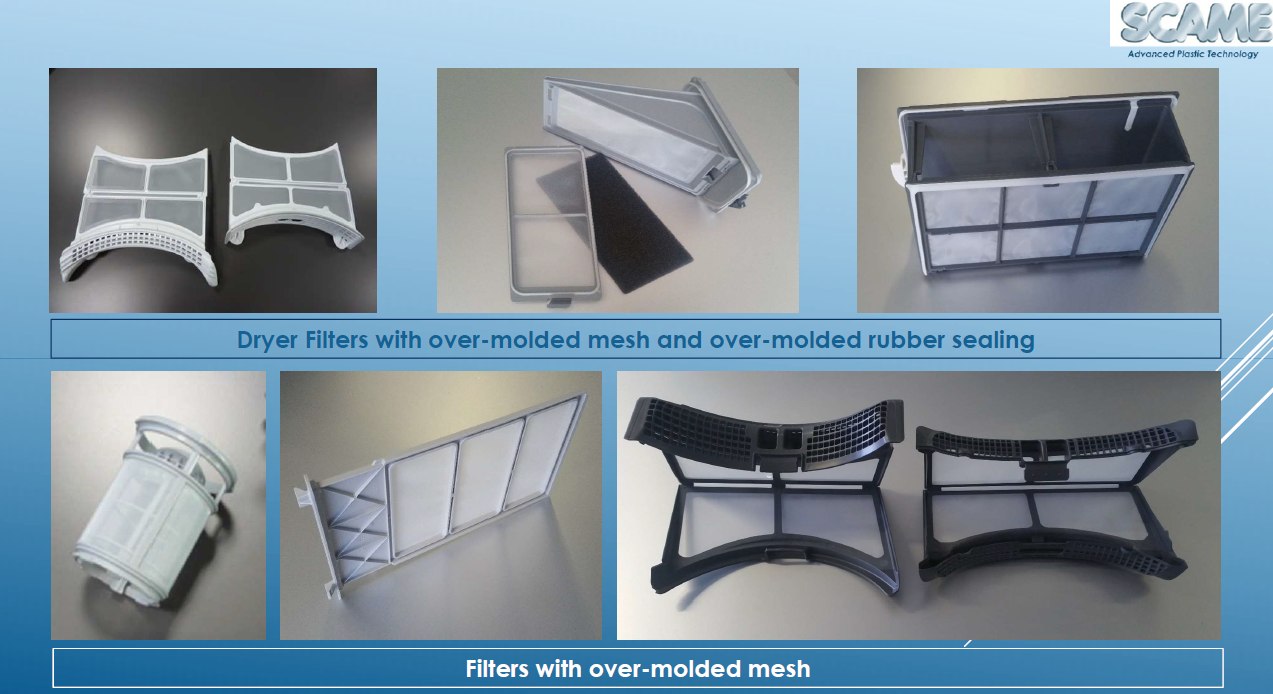
Metal or plastic meshes are placed and positioned in the mould cavity before injection, with automatic in-line seal testing and dimensional repeatability across large batches. The capability originated in household appliances — dishwashers and tumble dryers — and has since been transferred to six verticals: HVAC, professional coffee, medical, water management, safety and instrumentation.
It is an example of how technology transfer works inside the Group: a capability developed in a mature sector becomes an advantage in higher-margin ones.
The part leaves our facility finished, not requiring further processing.
Decoration, finishing and assembly
Finishing has been part of what Scame Mastaf does from the very beginning, and it is one of the reasons long-standing customers have never moved the work elsewhere. Spray painting, screen printing, multi-colour pad printing, heat transfer decoration, hot foil stamping and laser marking are all carried out in-house. Where the design allows, decoration takes place inside the mould and the downstream operation disappears altogether.
On assembly we go beyond the single part. Three welding technologies — ultrasonic, vibration and hot plate — cover everything from small components to large-format parts, sealed joints included. Downstream comes the sub-assembly of complete units that include bought-in parts: fasteners, inserts, gaskets, metal elements. What we deliver is not always a moulded part: often it is a finished unit, ready to go straight onto the assembly line, with one part number and one supplier accountable for it.
Every operation kept in-house is one handover fewer between two companies, days saved in transport and waiting, and a single party accountable when something goes wrong. On a decorated component entrusted to an outside finisher, an appearance defect shows up downstream and opens the usual argument about who answers for it. Here it does not.
Decoration and marking:
spray painting · screen printing · multi-colour pad printing · heat transfer · hot foil stamping · laser marking · in-mould decoration (IMD)
Assembly:
ultrasonic welding · vibration welding · hot plate welding · sub-assembly of units including bought-in parts
Image Gallery